You are using Internet Explorer and will not be able to use our website properly. Please change to an up-to-date browser for ideal presentation of the website.
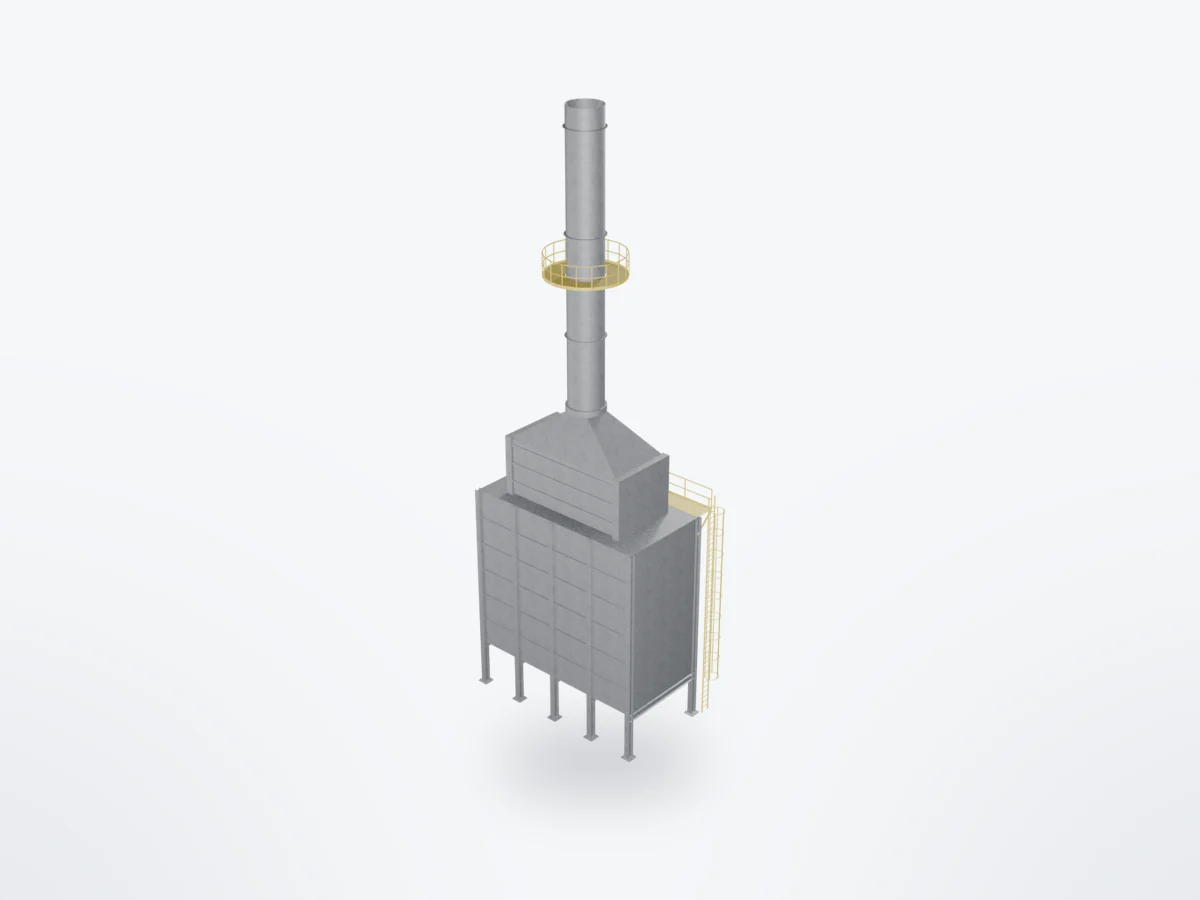
Combustion chambers fabricated to the licensor’s design: rolled shell panels in bolted courses on a column and ring-beam base, drilled, trial-assembled, insulated and packed for export in our own works.
Diameter, height and the number of courses follow your flare.
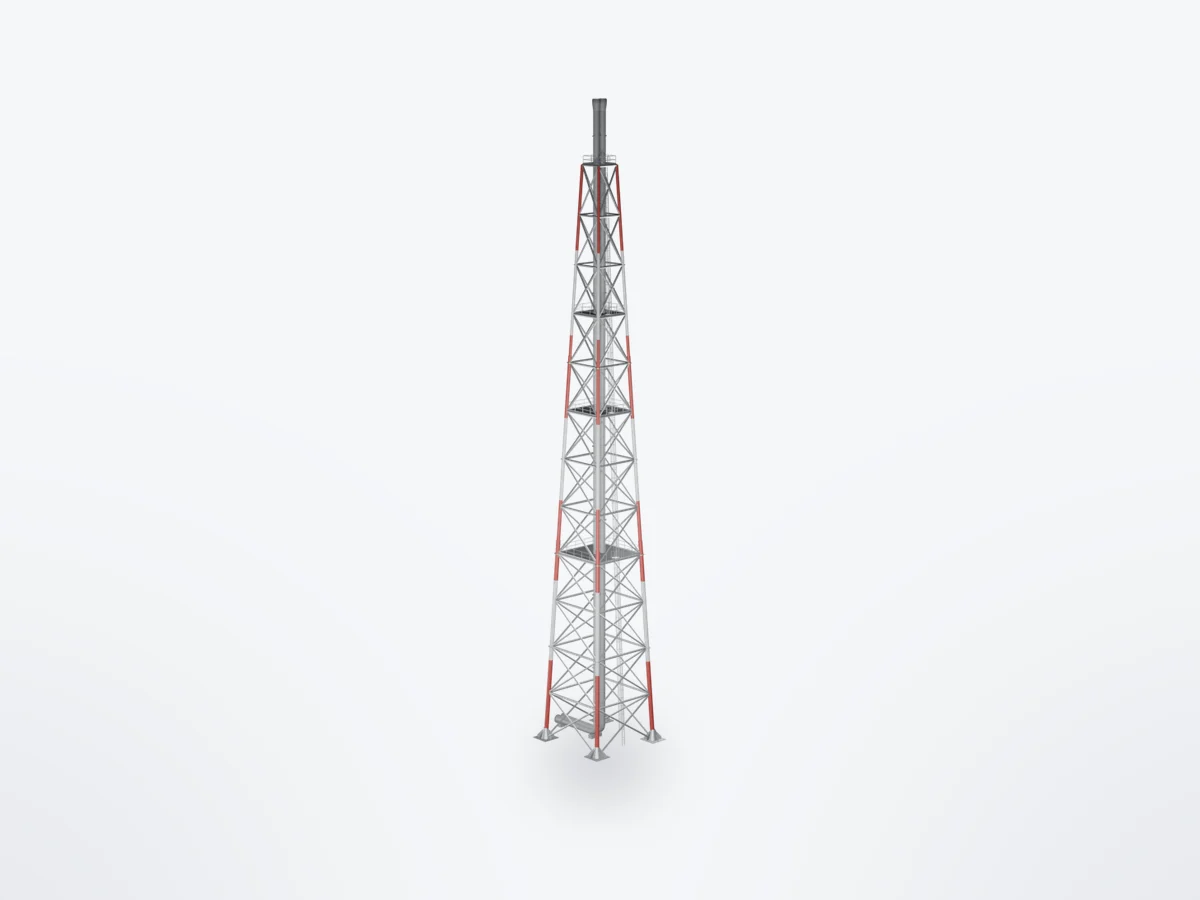
A chamber is a stack of rolled courses on a column base. More courses make it taller; more panels to the ring make it wider. The model shows one chamber as we built it. Yours is fabricated to the licensor’s drawings for your duty.
20 m
chamber diameter, Louisiana
46 m
chamber height, Louisiana
50 m
chamber height, Hazira
550 T
each chamber, 4 built
Explore the model
How it is built.
Scroll: the camera moves to each part in turn and ends on the exploded view. Drag to turn it round yourself.
Loading model0%
01 / 11
An enclosed ground flare, as we build it
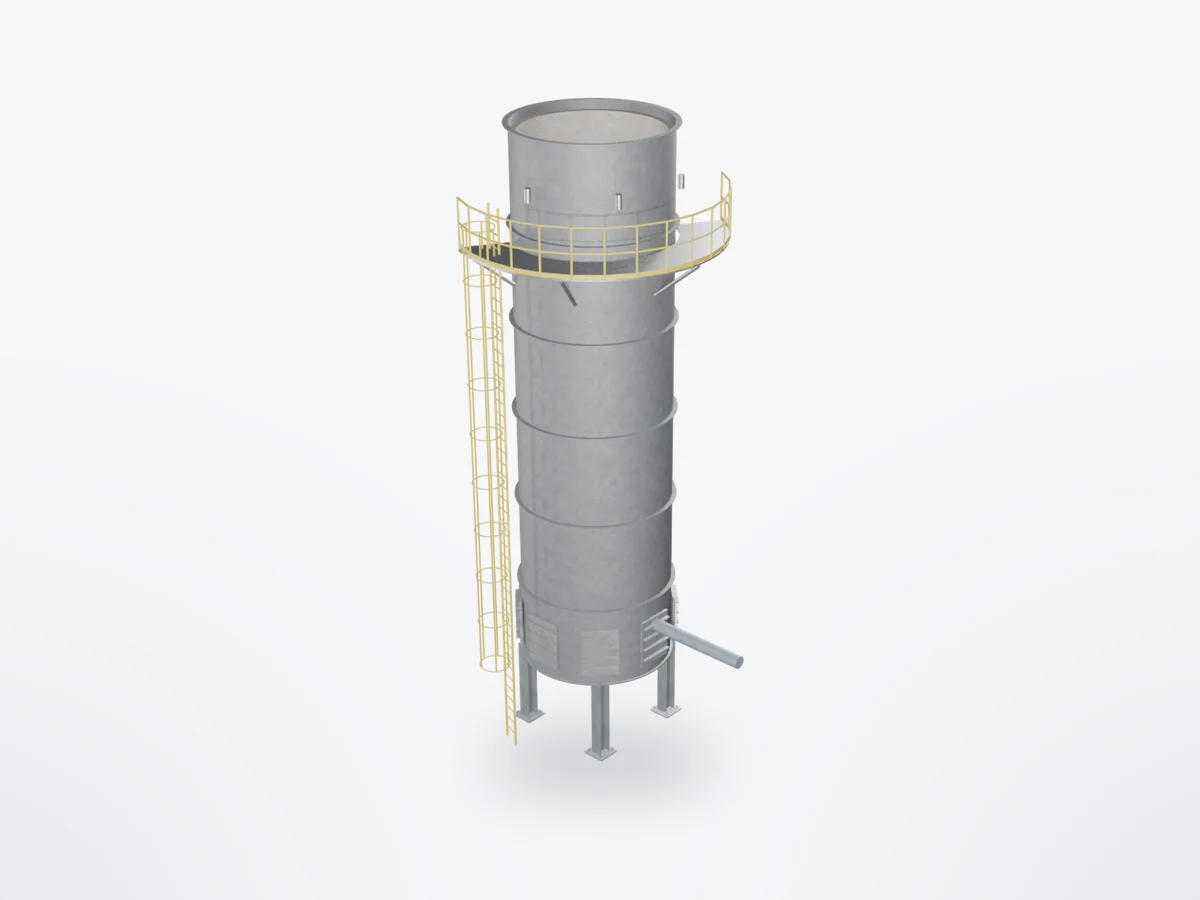
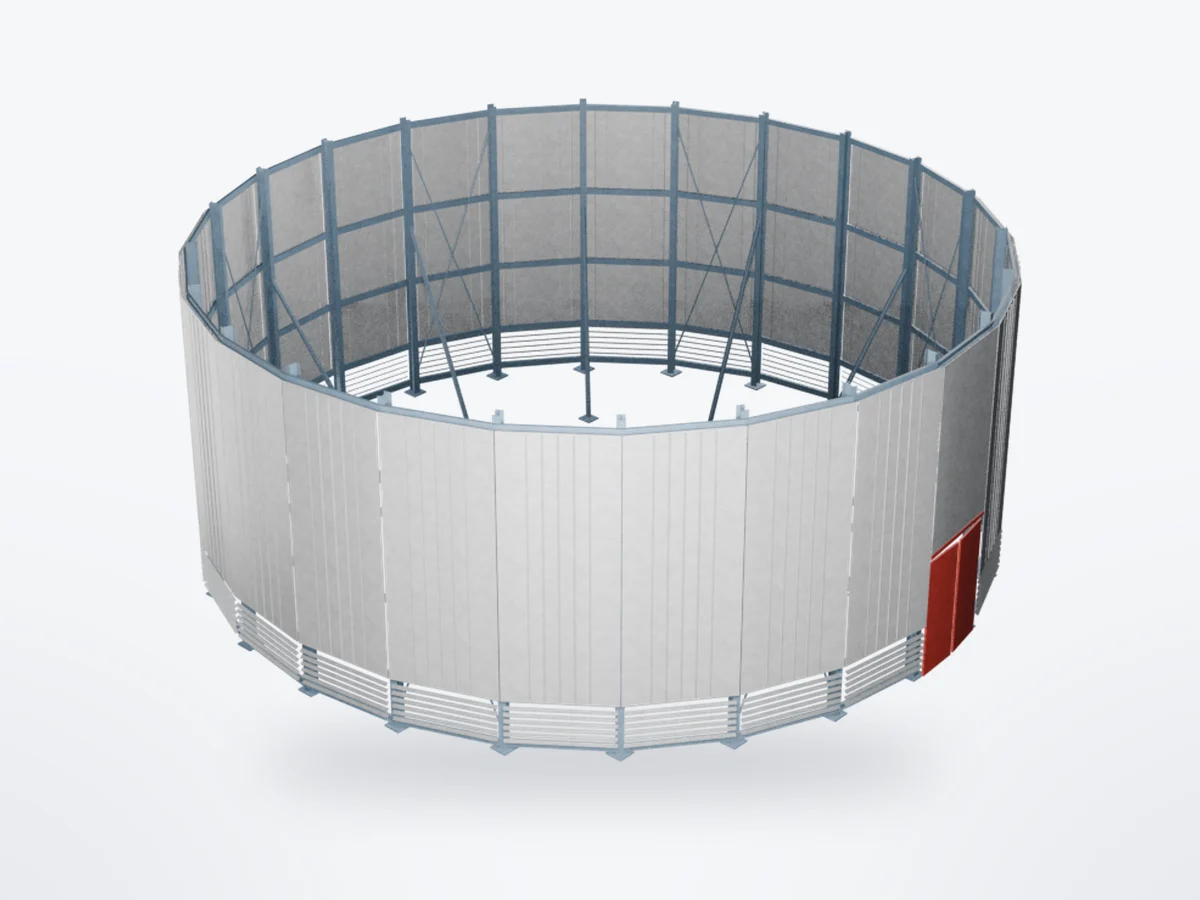
The design is the licensor’s. What we show here is how the steel is made: a column base, a shell of rolled panels in bolted courses, a wind fence and a noise shroud. The model is a typical arrangement, not a client’s drawing. The chambers we built are about 20 m across and 46 m high.
Scroll to see how it is built · drag to turn it round
02 / 11
The bottom section
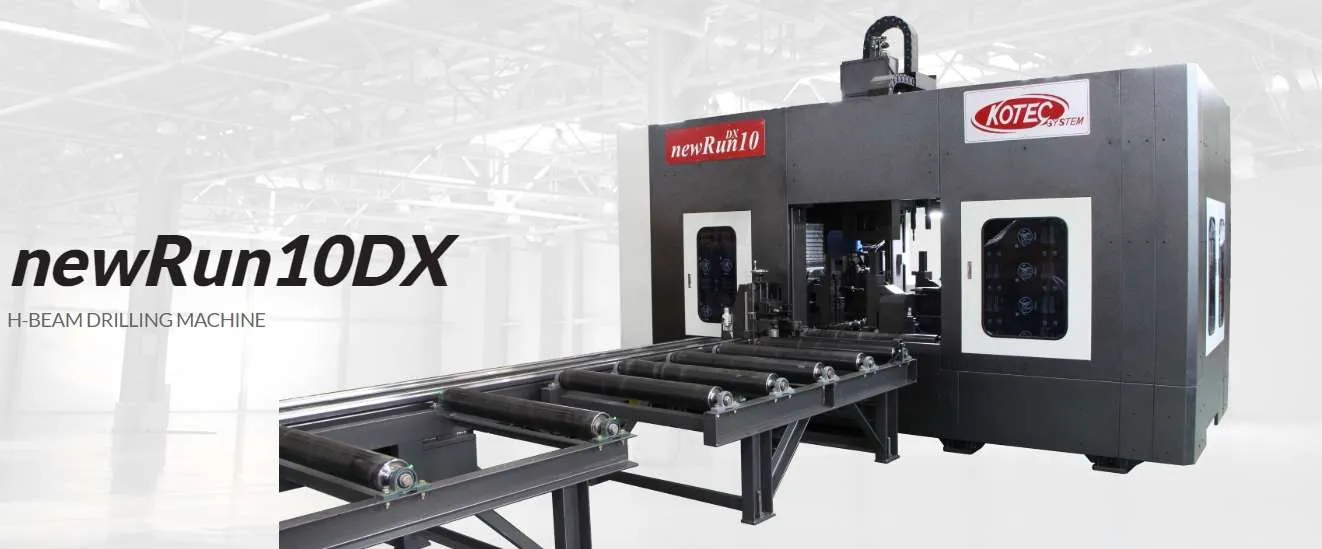
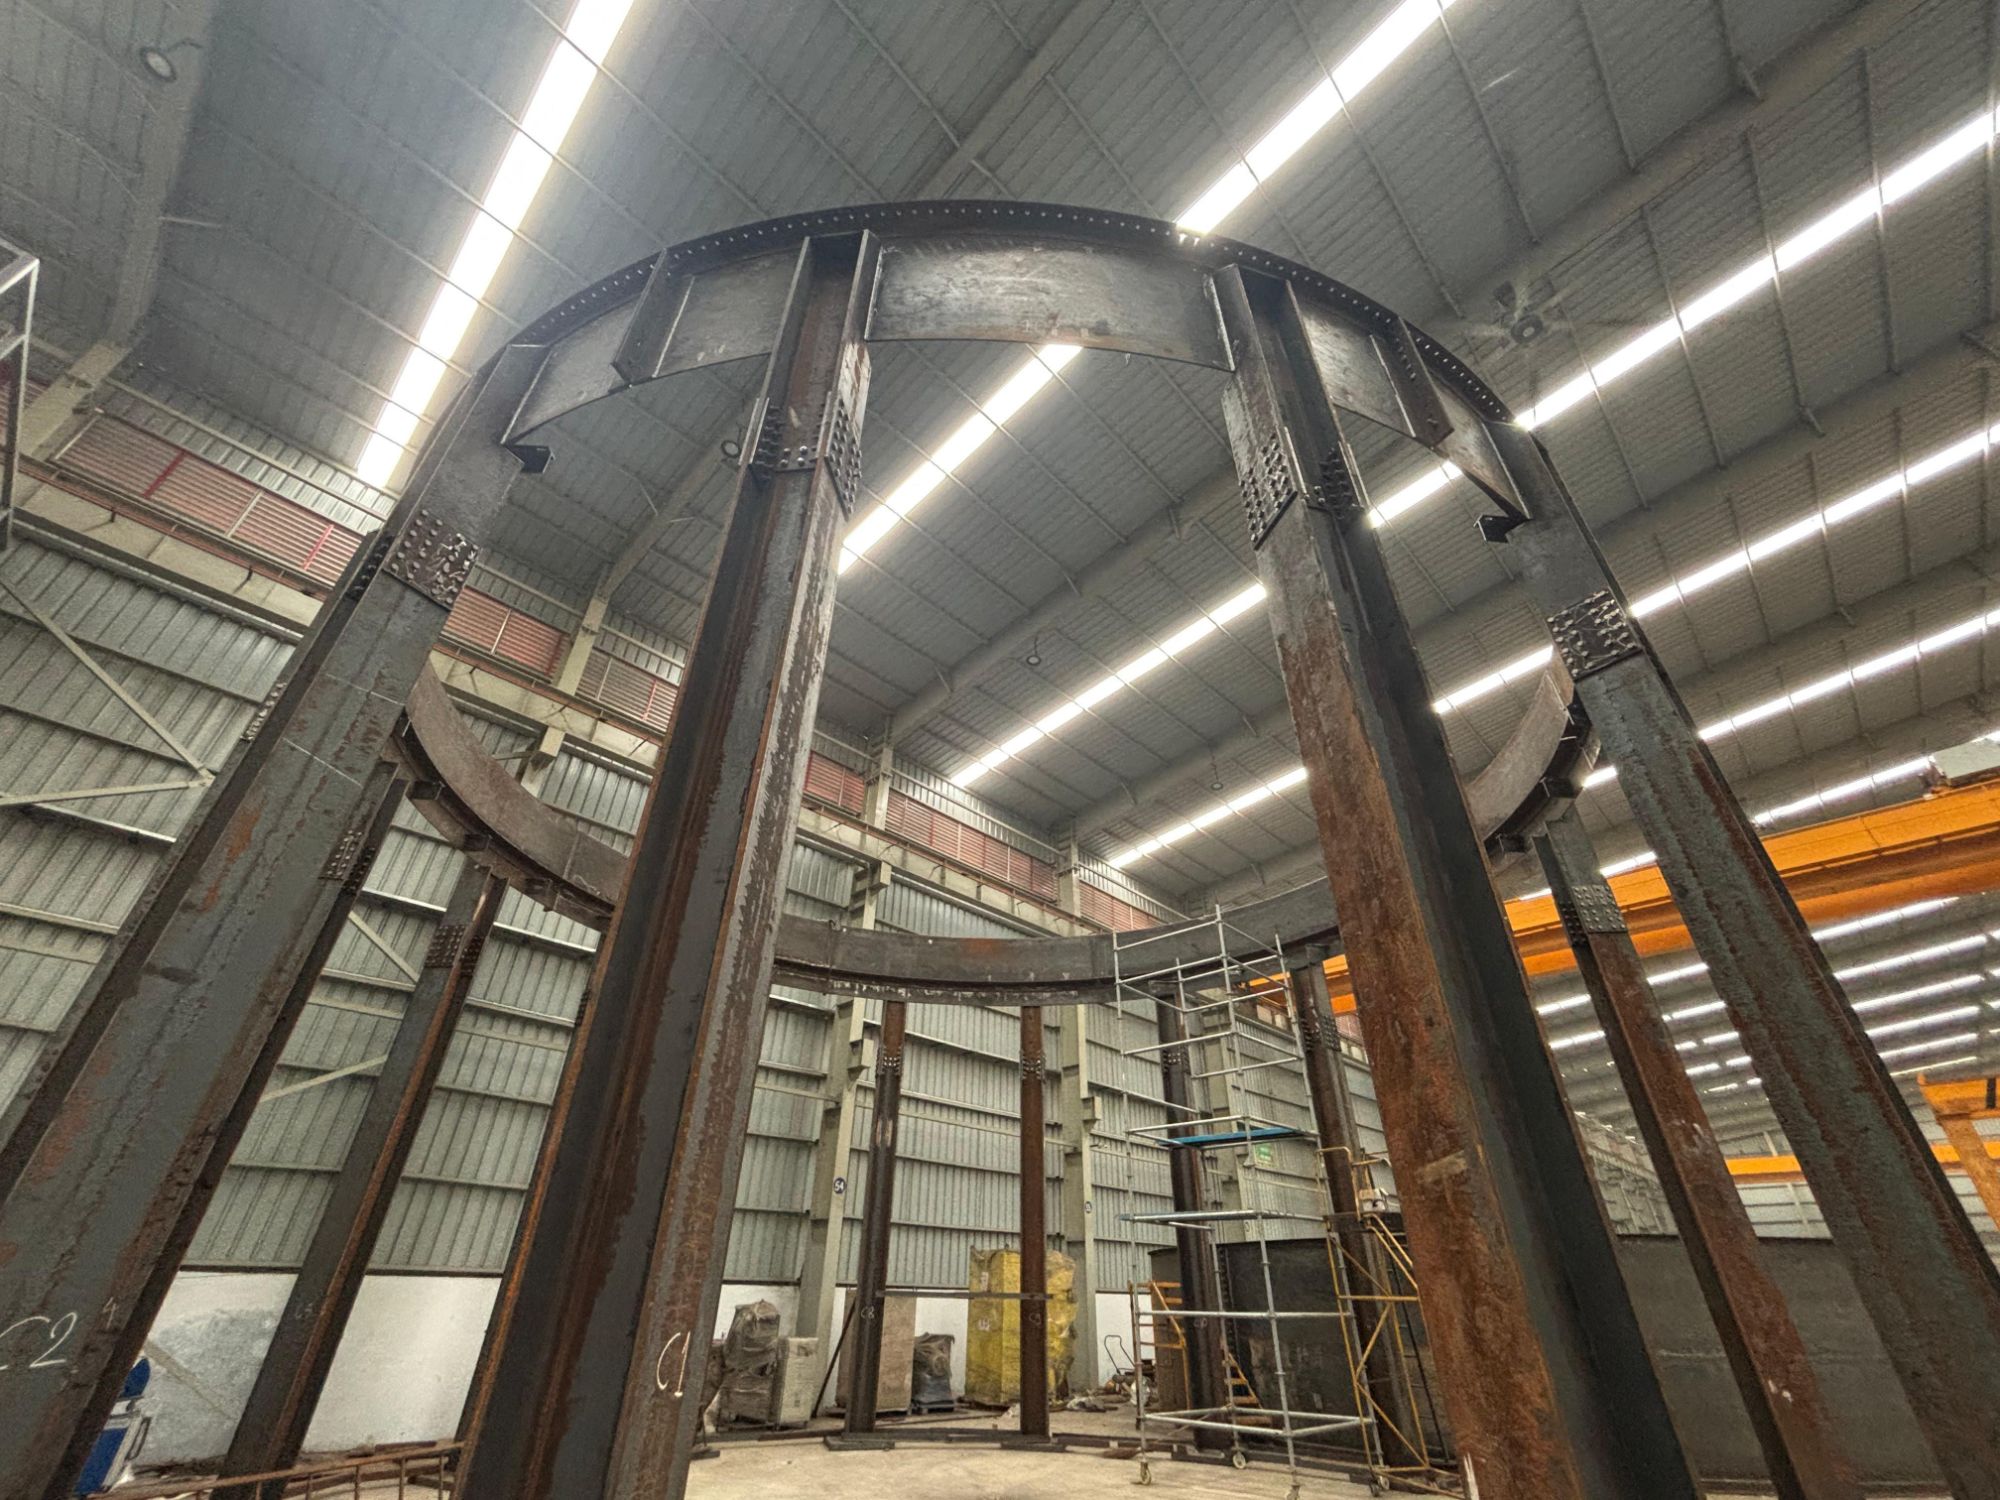
A ring of columns stands at the shell line, from base plates to a bolted splice, tied at the top by a curved ring girder. Each column has a stainless heat shield facing the burners. Holes in heavy profiles need more accuracy than plasma can give, so they are drilled on our Kotec CNC beam line, 3 faces in one pass.
How is it possible at Allmarc?
Used here for: The bottom section
Heavy profiles that need precise holes, where plasma cannot do the job: the lower structure and panel borders of a ground flare, and every bolted PEB and multi-storey frame.
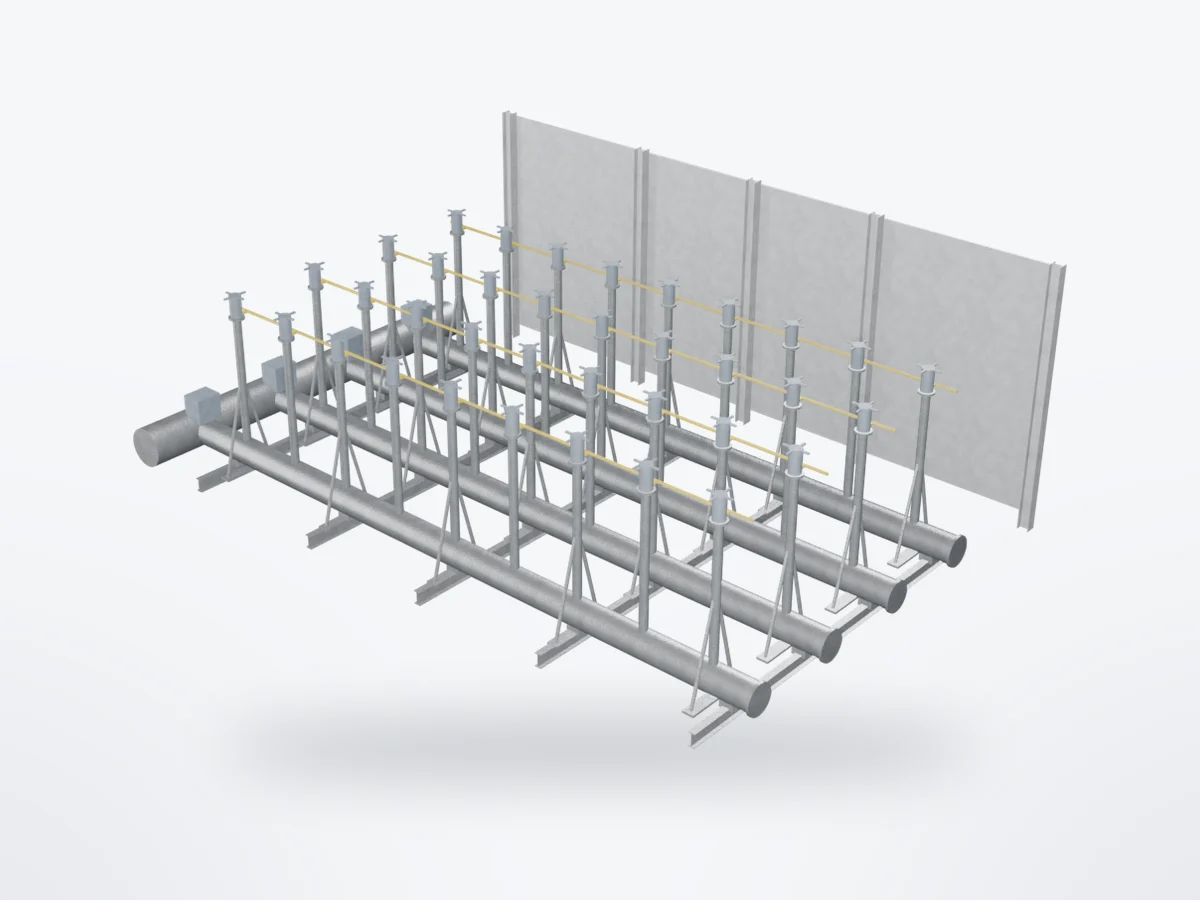
The chamber floor is plate on parallel floor beams that span the ring girder, with a framed window over each burner row. Runner pipes at grade feed risers up through the windows. The burner design is the licensor’s.
How is it possible at Allmarc?
Used here for: Bottom plate and burner plate
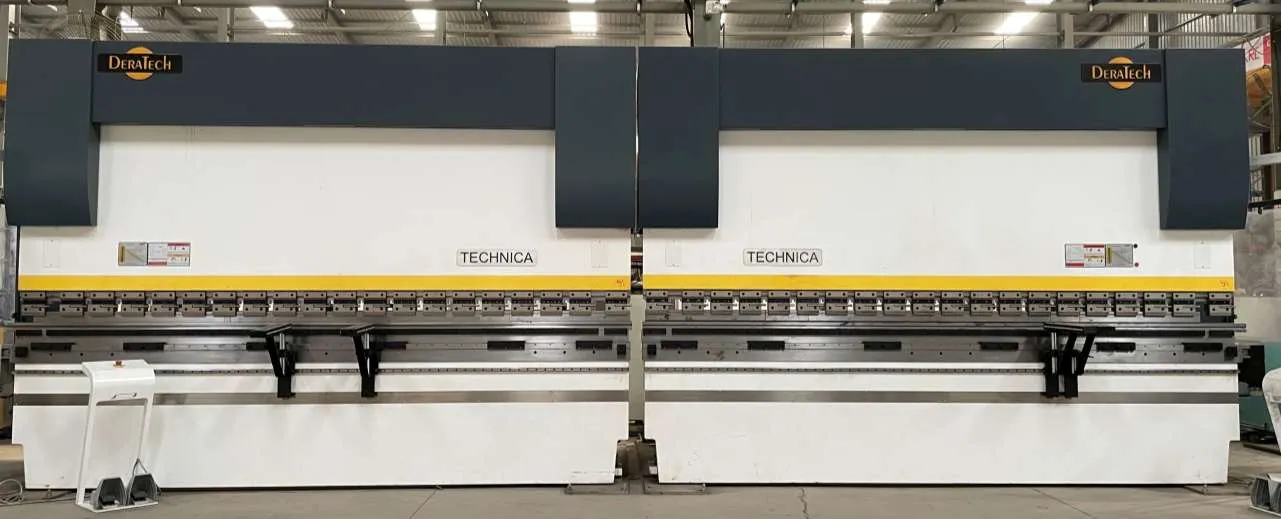
In 2024 we were the only buyer of Deratech’s 20 kW, 12 m laser.
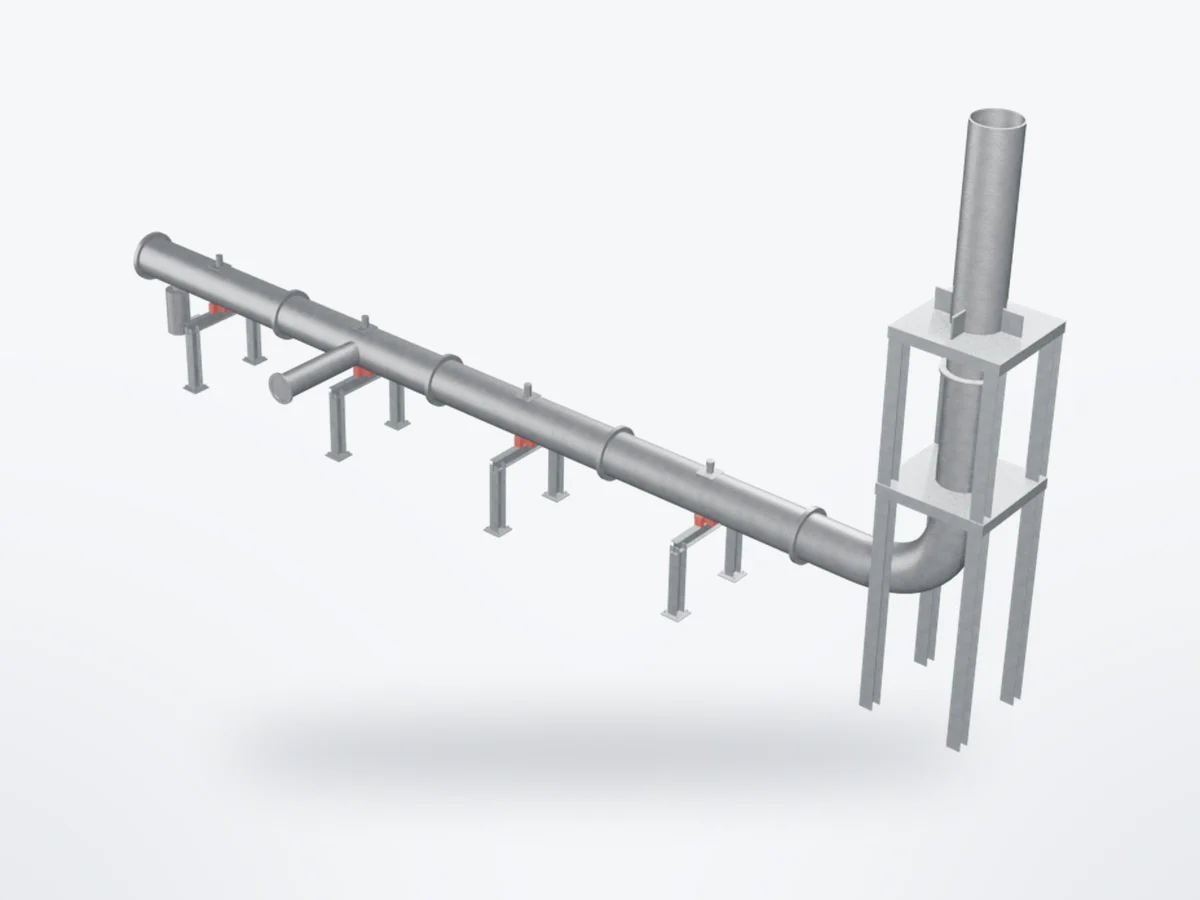
Shown for context: a gas header and valved stage lines running in under the fence to the burner rows, crossed by a grated walkway with a stair at each end.
05 / 11
The shell starts
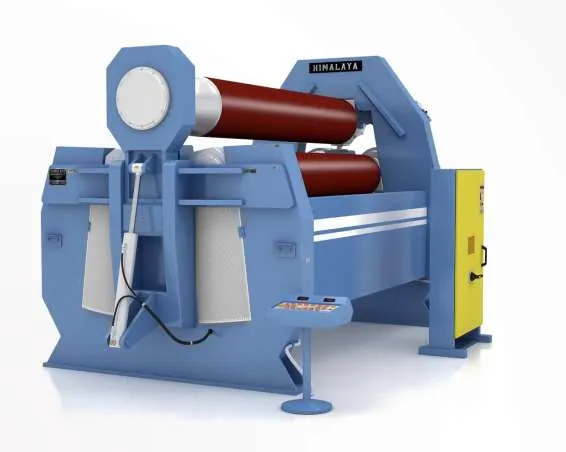
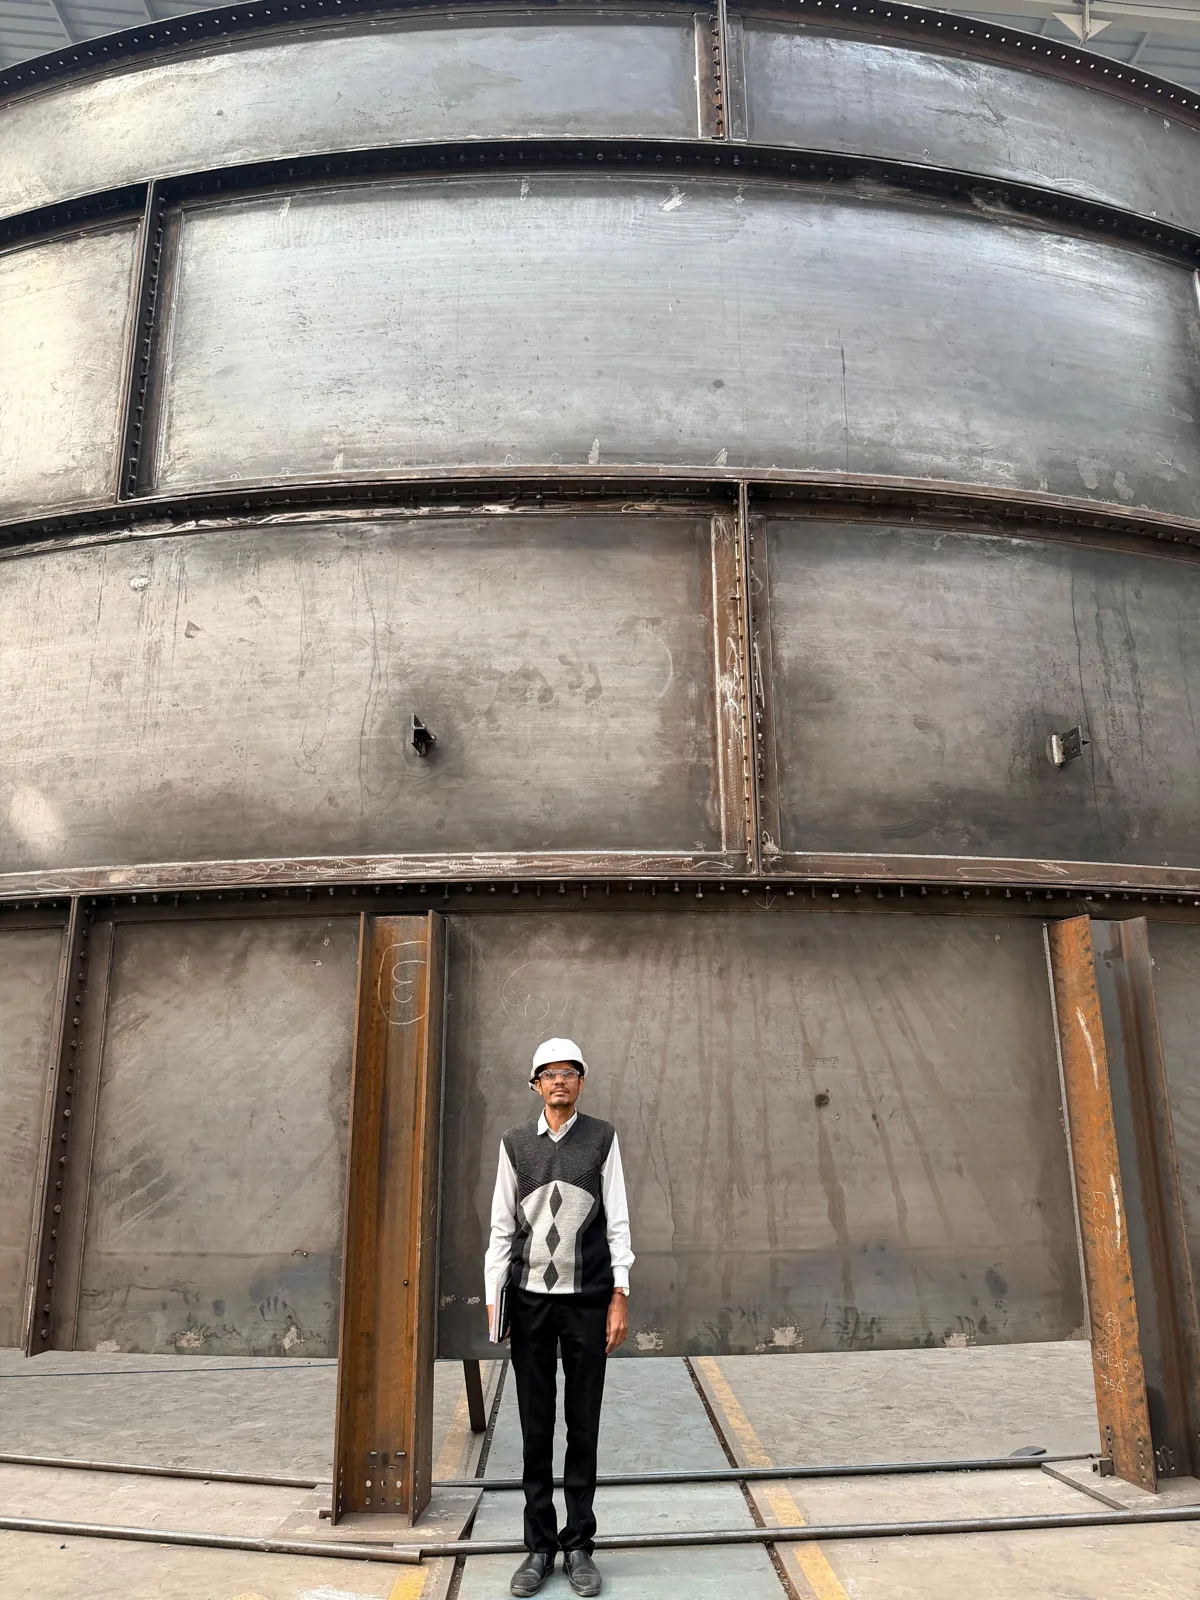
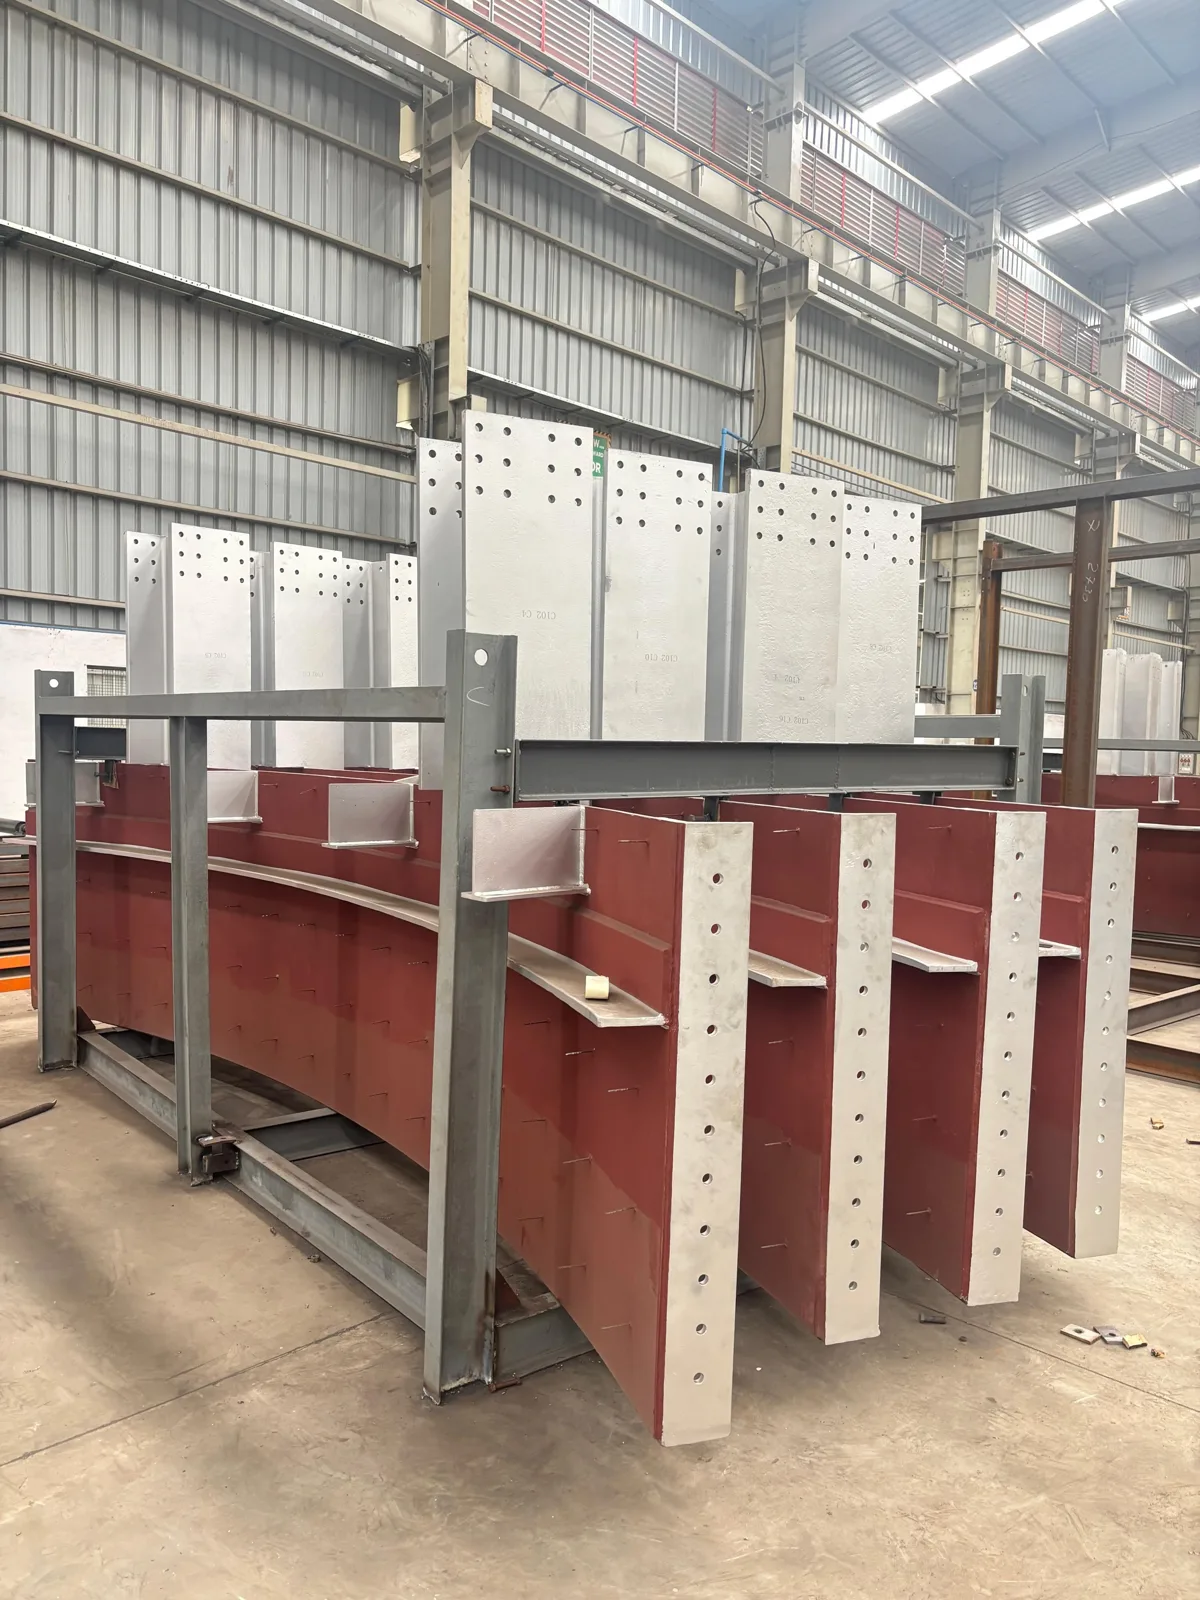
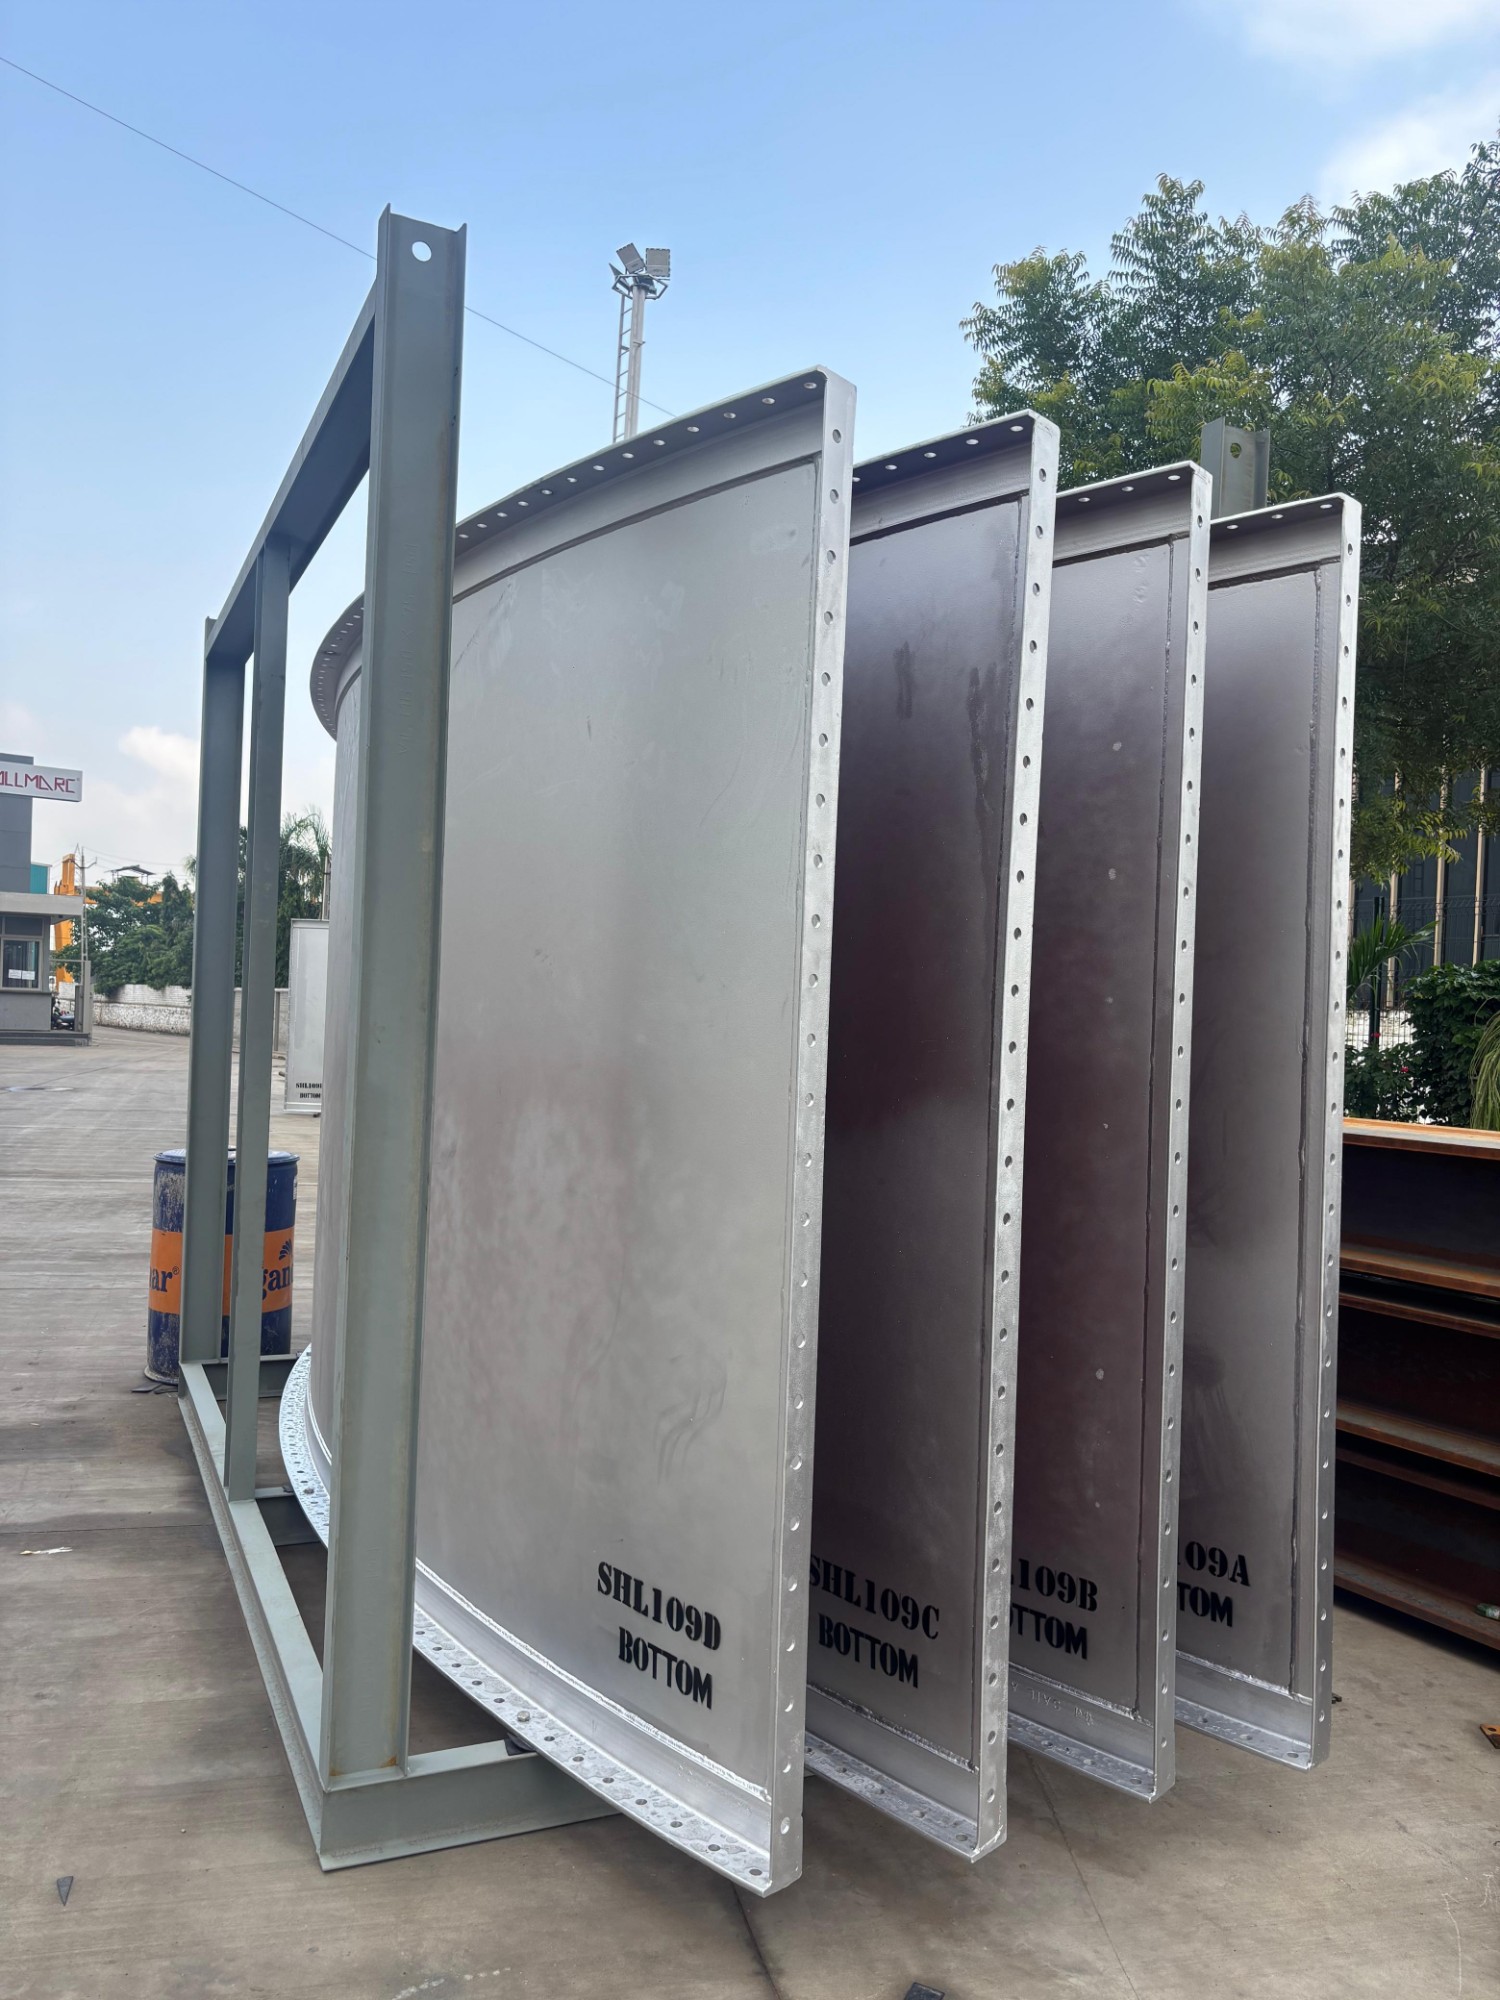
The lowest courses carry the most load and the noise shroud, so they use the heaviest plate. Each ring is made of curved panels with a bolted flange on every edge.
How is it possible at Allmarc?
Used here for: The shell starts
In 2024 we were the only buyer of Deratech’s 20 kW, 12 m laser.
The shell climbs course by course, with the vertical joints staggered from one ring to the next. Plate gets thinner as it climbs. Every panel is cut, rolled and numbered by ring and position.
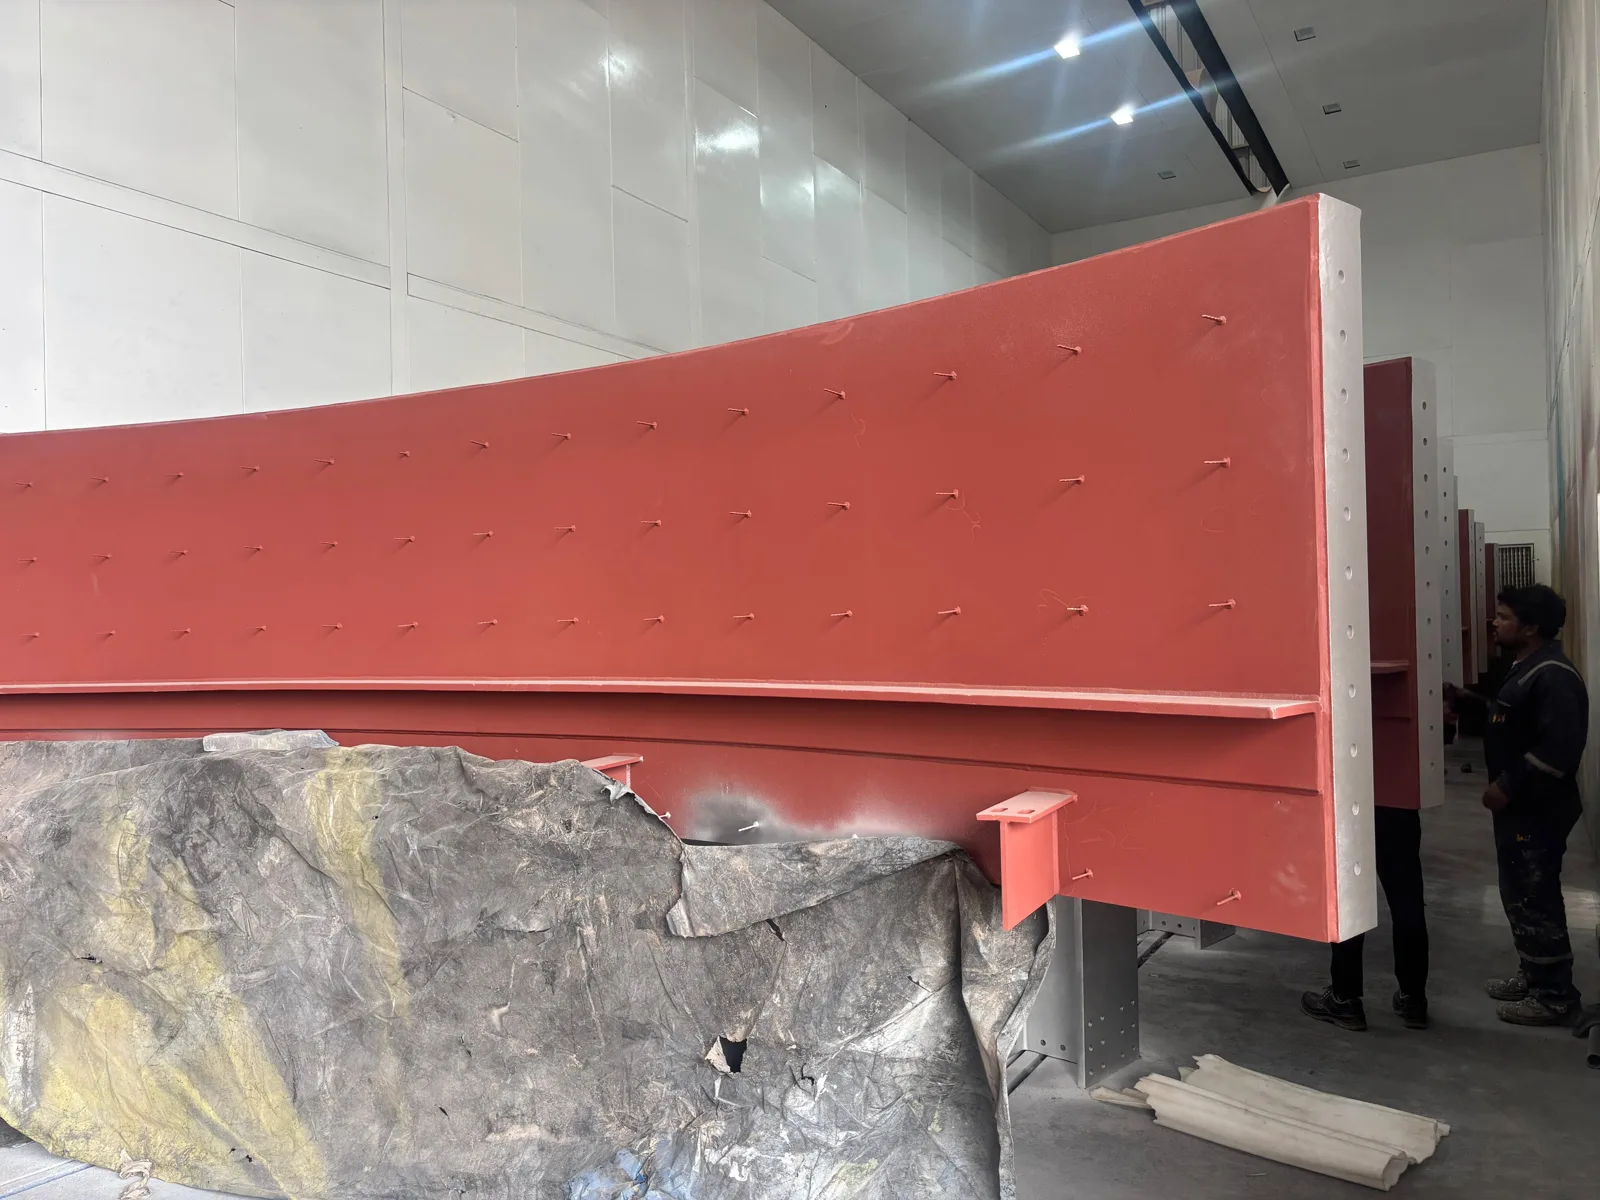
A rolled angle ring closes each course joint and is bolted all the way round. Studs are welded to the panels and the lining is applied in our works, so panels leave finished.
Straight panels between columns form a many-sided fence round the burners. The lower part is a flat insulated face with access doors; above it, sloping louvres let air in and keep the flame out of sight.
A lined enclosure hung clear of the ground on braced frames, so air still enters below it. Its wall is ribbed plate in panels between posts, and its roof is plate with standing seams, rising to land on the shell.
10 / 11
100% trial assembly
Every panel is assembled and inspected in our bay so that not one hole mismatches on site. On this project the chamber was trial-assembled four levels at a time; how many levels go up together depends on each project.
Bay: 30 m wide, 11.5 m under the hook
This project: 4 levels per set-up
11 / 11
Coated, packed, shipped
A Level 2 coating inspector is on the floor full time; weather is checked and a test run before every batch of paint. The export packing method was developed by our own team.
How is it possible at Allmarc?
Used here for: Coated, packed, shipped
A Level 2 coating inspector on the floor full time; weather checked and a test before every batch of paint.